Standard part and Figure
Which part of ISO 80369, and which Figure or drawing the item is made against. The Figure is what fixes the limits, not the photograph.
A gauge carries its tolerance in two places: the turned conical form and, where one is present, the thread. This page describes the sequence that produces both, states which step fixes which part of the tolerance, and separates what is confirmed per order from what this page does not claim.
Include the standard part, the Figure or drawing revision, the material and treatment, the critical feature, the quantity and the inspection or calibration documents you expect. Those five inputs are what let a manufacturing question be answered instead of estimated.
Each of these changes what has to be machined and what has to be measured afterwards, so they belong in the inquiry rather than in the purchase order.
Which part of ISO 80369, and which Figure or drawing the item is made against. The Figure is what fixes the limits, not the photograph.
The material and any heat treatment must be stated before grinding, because the final size is set after treatment rather than before it.
The conical form, the thread, a specific diameter or another named feature. Which feature is critical decides which inspection step has to follow.
The inspection record, calibration statement, traceability information and protective packaging that should accompany the item.
Three illustrations place the manufacturing steps in order: turning produces the conical form and its surface, grinding sets the thread flank and the final size after heat treatment, and the finished item then passes dimensional and thread inspection before packing. The sequence matters because each step fixes a different part of the tolerance, and a dimension that is lost at grinding cannot be recovered at inspection.
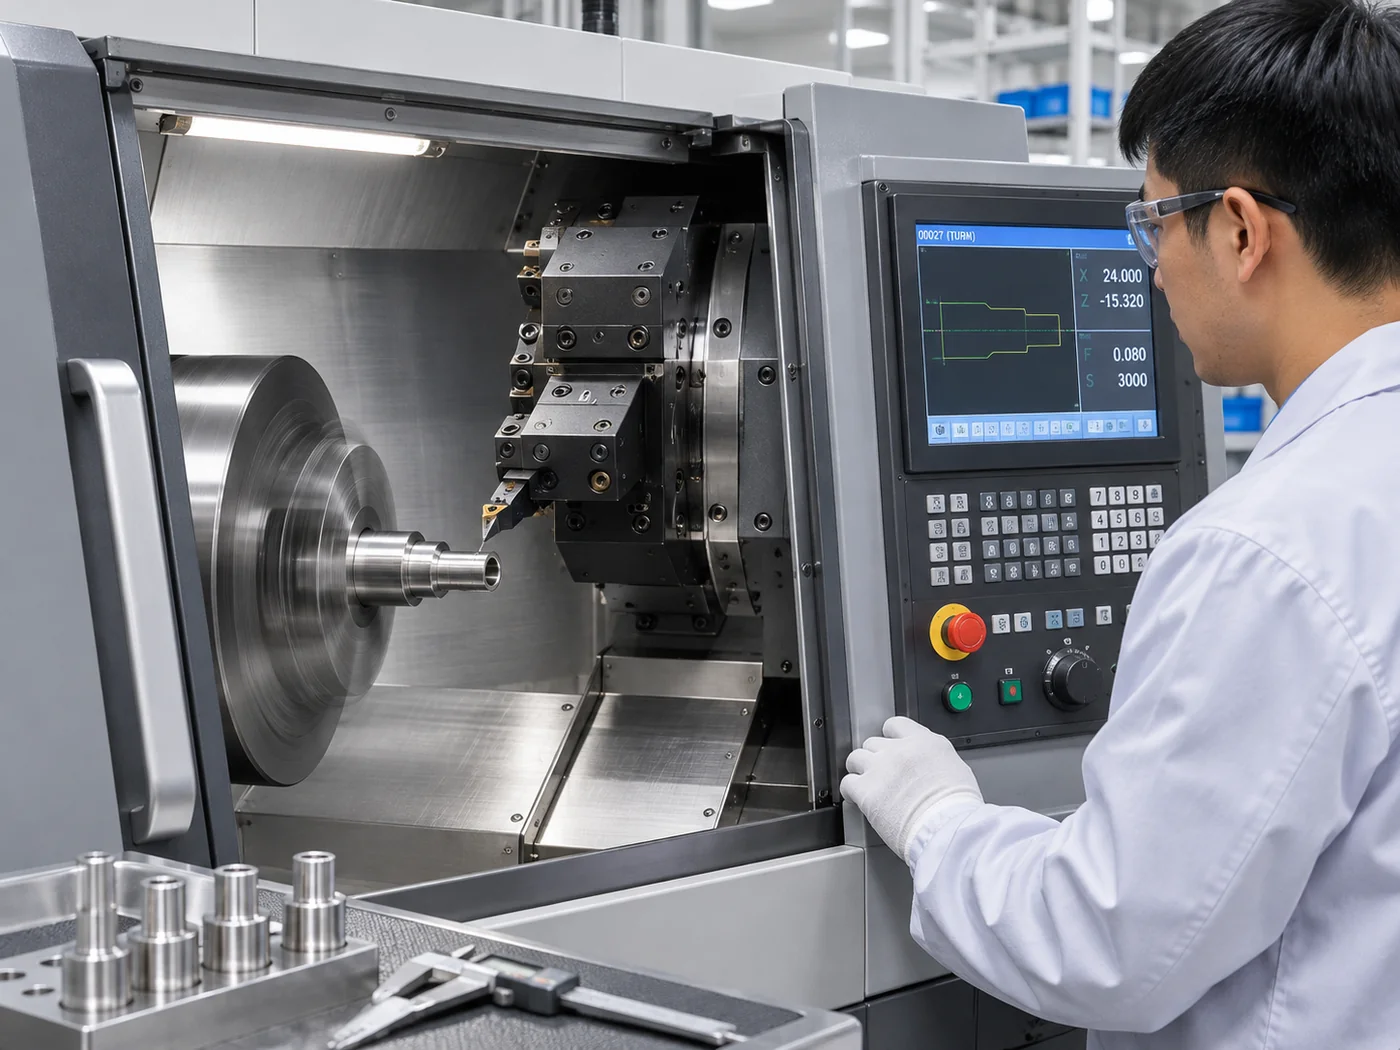
Illustrative turning of a gauge blank, where the conical form and its surface finish are produced. The machine and control screen are generic and no machine model is depicted.
Luer gauges produced to these tolerances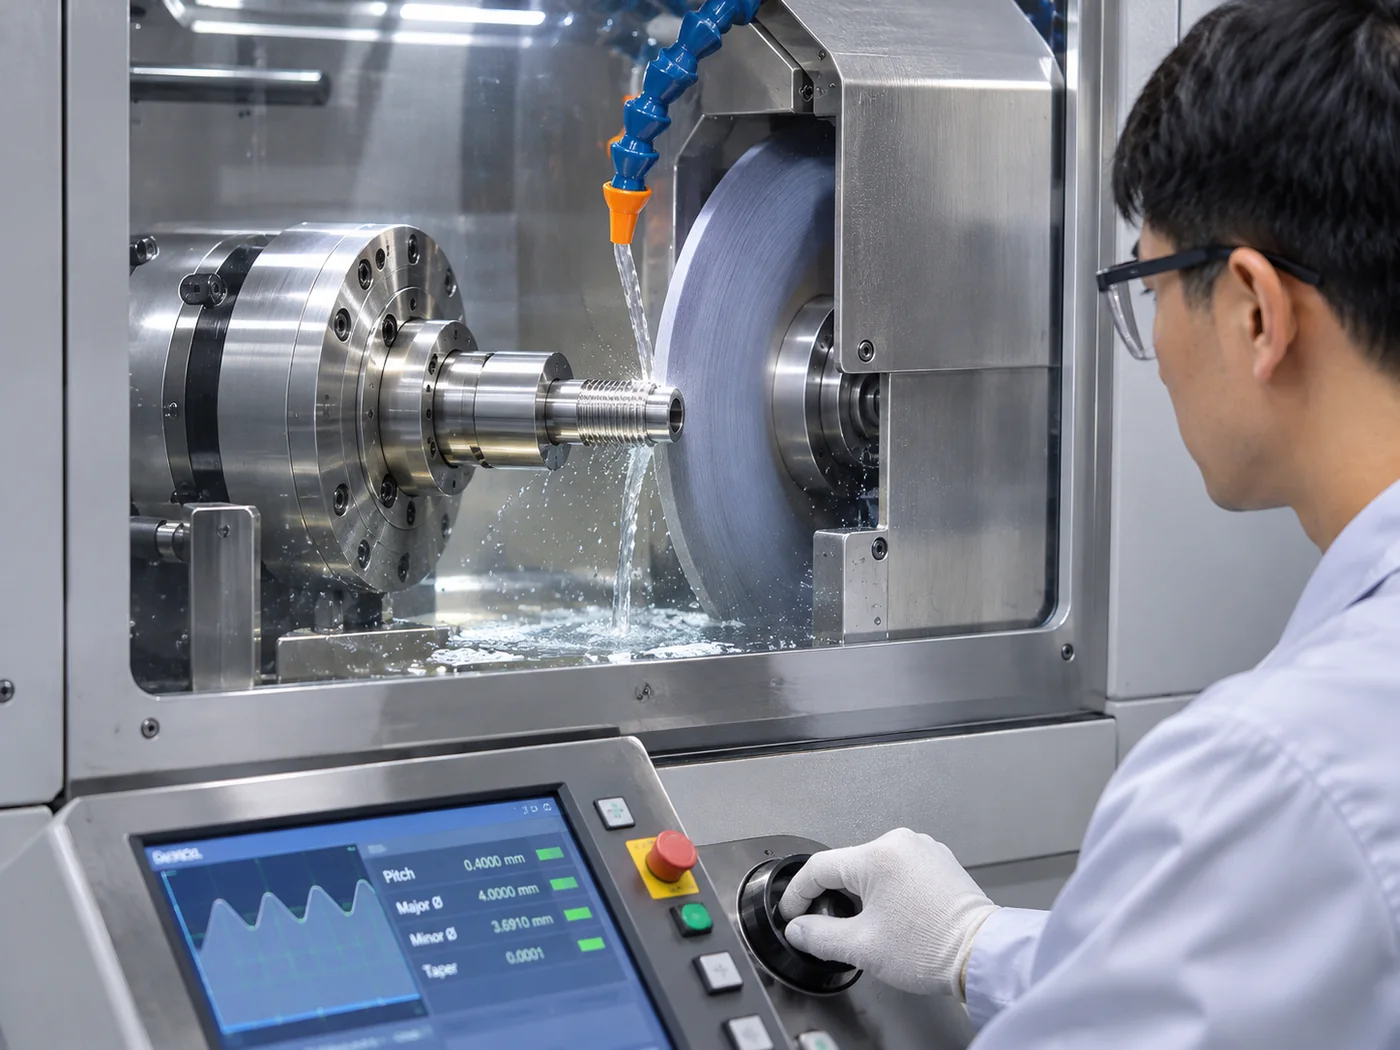
Illustrative thread grinding after heat treatment, where the thread flank and the final size are set. The wheel and machine shown are generic.
How the finished feature is verified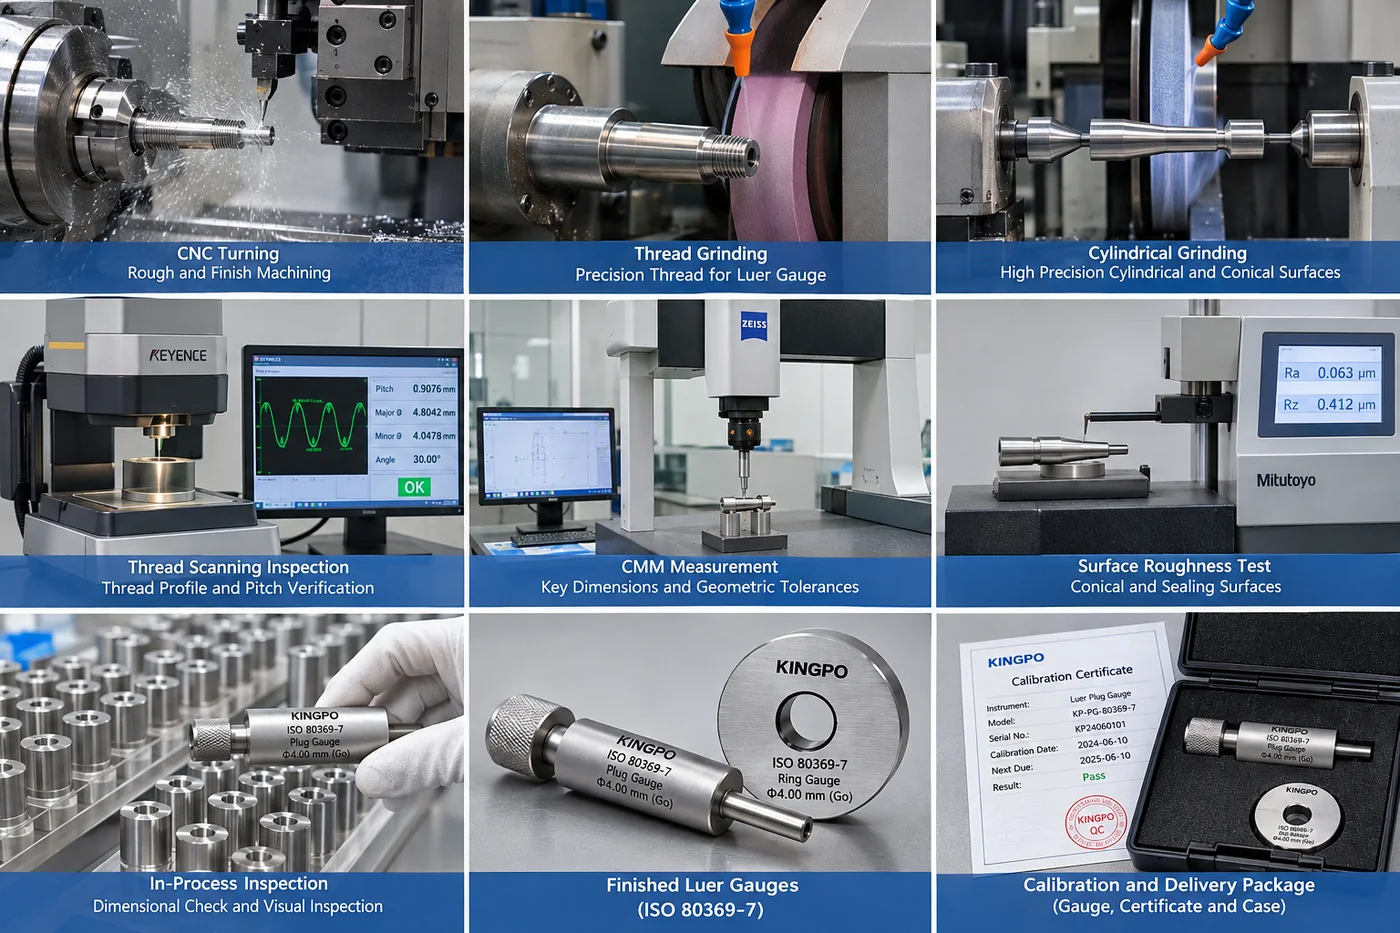
Illustrative full workflow from machining through inspection to packing. Labels and values embedded in the graphic are schematic and are not specifications.
See how verification is organizedA dimension lost at grinding cannot be recovered at inspection. The sequence below is why the inspection plan follows the process plan rather than replacing it.
Produces the conical form, the primary diameters and the surface finish. The cone angle comes from this step, and re-cutting it later risks the seating geometry.
Sets the thread flank and the final size once the part has been hardened. Grinding allowance has to be planned before treatment, not after it.
The finished feature is measured against the drawing or Figure, the result is recorded against the item, and the part is packed with its documents.
A manufacturing page is only useful if a buyer can tell which sentences are commitments and which are not. The two lists below are the boundary.
Material, heat treatment, grinding allowance, inspection method, inspection record, calibration wording, packaging and delivery are all confirmed against the exact item and quantity, not inherited from a general statement on this page.
Calibration and documentsManufacturing questions usually turn into either a verification question or a selection question. Both are covered on the pages below.
How checks are organized by product type, and what evidence is available for each.
Plug, ring and lock gauges, and how a set is selected against a standard part.
How to read a gauge requirement before ordering, including which feature decides the gauge type.